Product Overview
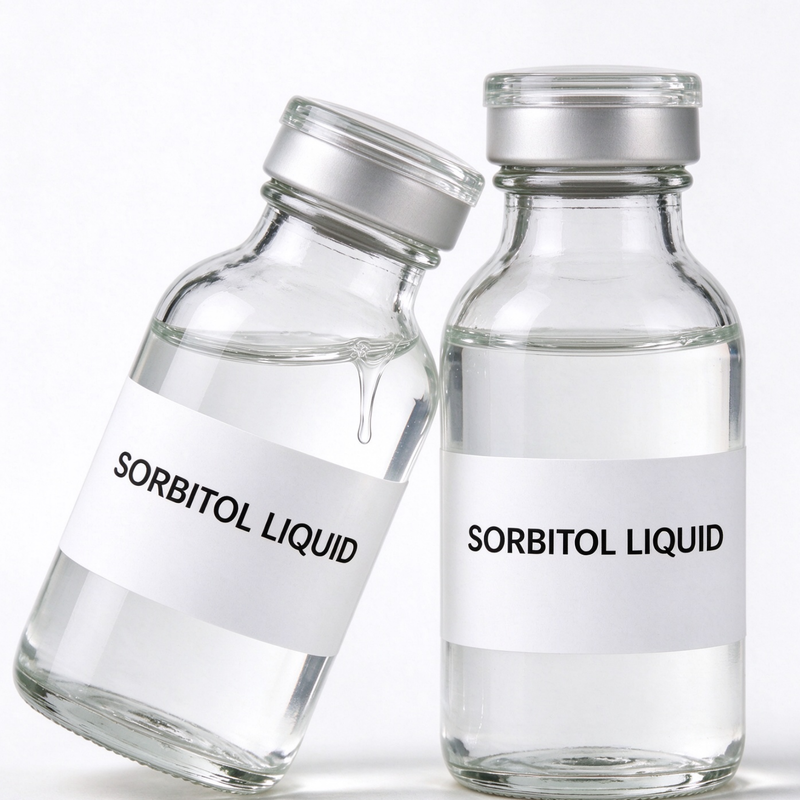
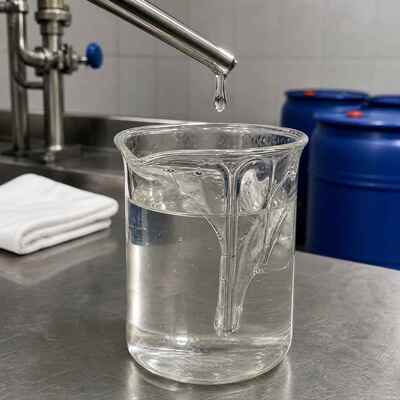
Our Sorbitol Solution 70% is a clear, colorless, and odorless syrupy liquid with a clean, mildly sweet taste, manufactured to food-grade standards for use across a wide range of food and beverage applications. Chemically identified as D-Glucitol (E420, INS 420(ii)), it is a sugar alcohol polyol that functions as a sweetener, humectant, stabilizer, and bulking agent in food formulations.
Supplied as an aqueous solution with a dry substance content of approximately 70%, this product meets the requirements of major international standards including FCC (Food Chemical Codex), FAO/JECFA, and EU E420 specification. It is certified Halal and Kosher, making it suitable for import into markets with specific religious dietary requirements, including the Middle East, Southeast Asia, and Jewish communities worldwide.
Sorbitol occurs naturally in many fruits and vegetables, and commercially it is derived from corn or wheat starch through a catalytic hydrogenation process that converts glucose into sorbitol. This process is entirely plant-based and contains no ethanol or animal-derived ingredients, which is why sorbitol consistently receives Halal certification from recognized bodies.

Technical Specification
| Parameter |
Specification |
| Product name |
Sorbitol Solution 70% |
| Chemical name / CAS number |
D-Glucitol / 50-70-4 |
| E number |
E420 |
| Appearance |
Clear, colourless to pale straw viscous liquid |
| Assay (D-Glucitol, dry basis) |
70.0% min |
| Dry substance / water |
69.0-71.0% / 29.0-31.0% |
| pH (25 °C) |
5.0-7.5 |
| Density (20 °C) |
1.285-1.315 g/cm³ |
| Conductivity |
25 µS/cm max |
| Grade |
Industrial Grade |
Typical specification. The certificate of analysis issued for each shipment is the governing document.
Typical Certificate of Analysis
| Test item |
Typical result |
Method |
| Assay (D-Glucitol) |
70.3% |
HPLC |
| Appearance |
Clear, colourless |
Visual |
| Dry substance |
70.1% |
Refractometric |
| Water content |
29.9% |
Karl Fischer |
| pH (25 °C) |
6.3 |
pH meter |
| Conductivity |
9 µS/cm |
Conductivity meter |
| Reducing sugars |
0.06% |
Titrimetric |
| Iron (Fe) |
< 1 mg/kg |
ICP-MS |
| Total heavy metals (as Pb) |
< 5 mg/kg |
Colorimetric |
| Ash |
< 0.05% |
Gravimetric |
A certificate of analysis is issued for each lot against the drum number, and a safety data sheet is supplied with the shipping documents.
Key Features & Benefits for Food Applications
Multi-Functional Food Ingredient – Works as a sweetener, humectant, stabilizer, and thickener in a single product, simplifying your formulation and reducing the number of additives you need to manage.
Clean, Mild Sweetness – Provides approximately 60% of the sweetness of sucrose with a pleasant, cooling taste profile, ideal for sugar-reduced and sugar-free product formulations.
Excellent Moisture Retention – Helps keep baked goods, confectionery, and other food products fresh and soft by retaining moisture and preventing drying, cracking, or staling during storage.
Sugar-Free & Diabetic-Friendly – Sorbitol metabolism does not require insulin and does not raise blood glucose levels significantly, making it suitable for diabetic-friendly and reduced-calorie products.
Does Not Promote Tooth Decay – Sorbitol is non-cariogenic, making it a preferred sweetener for sugar-free chewing gum, mints, and oral care products.
Halal & Kosher Certified – Fully certified for import into Middle Eastern, Southeast Asian, and other markets requiring Halal compliance, as well as Kosher-certified for Jewish dietary requirements.
Consistent Food-Grade Quality – Every 250kg drum delivers a stable 70% concentration, clear appearance, and reliable performance that meets international food safety standards.
Bulk Supply Ready – Packed in sturdy 250kg drums with flexible wholesale arrangements, ideal for food manufacturers, distributors, and importers requiring steady supply.
Applications
sorbitol Solution 70% is widely used across the food industry as a versatile ingredient:
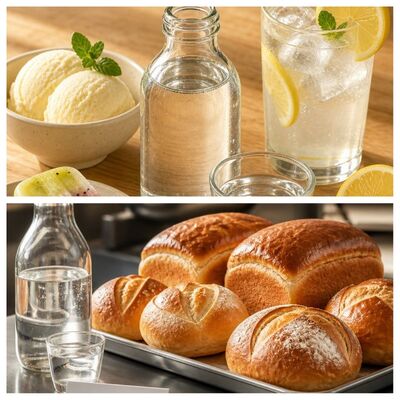
Confectionery – Sugar-free candies, chewing gum, mints, and chocolate products. Sorbitol provides sweetness without promoting tooth decay and imparts a pleasant cooling sensation.
Baked Goods – Cakes, cookies, pastries, and granola bars. Sorbitol retains moisture to keep products soft and fresh, and it does not participate in Maillard browning, helping maintain product color.
Beverages & Dairy – Flavored drinks, ice cream, frozen desserts, and dairy desserts. Sorbitol acts as a stabilizer and prevents crystallization in frozen products.
Health Foods – Sugar-free and reduced-calorie products, diabetic-friendly formulations, and low-glycemic food items.
Sauces & Condiments – Stabilizer and viscosity modifier in dressings, sauces, and condiments.
Meat & Seafood Products – Improves water retention, enhances flavor, and increases product yield in processed meat and surimi products.
Who Is This For?
Food manufacturers and processors
Food ingredient distributors and importers
Brands developing sugar-free, reduced-sugar, or health-conscious products
Buyers requiring Halal or Kosher certified ingredients for specific markets
Importers supplying the Middle East, Southeast Asia, and other Halal-sensitive regions
Quality Control
Quality is built into every stage of our production process, from raw material intake to final drum shipment. Our quality control system is designed to meet the expectations of international food manufacturers, importers, and regulatory bodies, and is aligned with the requirements of FCC, FAO/JECFA, and EU E420 specifications for sorbitol syrup.
Raw Material Control
• All starch raw materials (corn or wheat based) are sourced from approved suppliers with established vendor qualification records.
• Each incoming lot is tested for identity, moisture, and microbiological safety before being released to production.
• Certificates of analysis from raw material suppliers are retained and cross-referenced with internal batch records for full traceability.
• Materials that do not meet incoming specifications are rejected and segregated to prevent accidental use.
In-Process Control
The production of sorbitol involves catalytic hydrogenation of glucose syrup under controlled temperature and pressure. Critical process parameters are monitored and recorded throughout the reaction:
• Hydrogenation reaction: Temperature, pressure, and reaction time are controlled within validated ranges to ensure complete conversion of glucose to sorbitol and minimize residual reducing sugars.
• Catalyst management: Nickel catalyst is carefully handled and removed through filtration and purification steps. Residual nickel levels are monitored as a critical safety parameter.
• Purification: Ion exchange and filtration steps are controlled to remove ionic impurities, color bodies, and any residual catalyst fines.
• Concentration: The final solution is adjusted to the target dry substance content (69.5–70.5%) under controlled evaporation conditions.
Intermediate samples are taken at key process points and tested for dry substance, pH, and sorbitol content to confirm the process is proceeding within specification before the batch advances to the next stage.
Packaging & Shipping
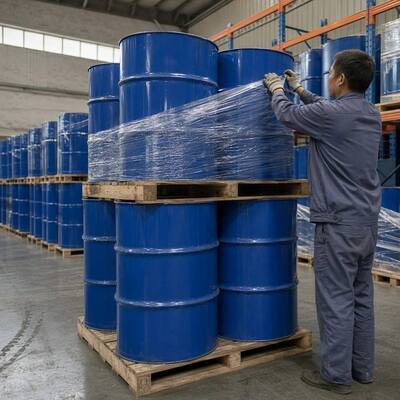
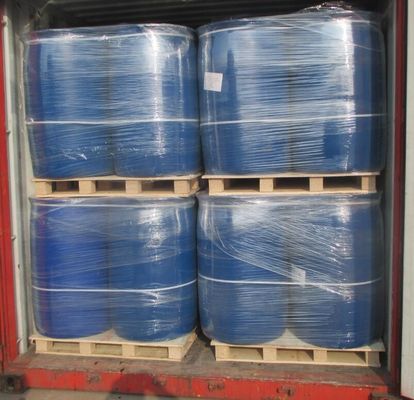
For a finishing line the drum is the working unit: 250 kg net in a blue tight-head drum, both bungs sealed, label carrying product, grade, net weight and lot number. Four drums make a pallet with corner boards and shrink wrap, and 80 palletised drums complete a 20 ft load. Mills that dose finish from a bulk tank can order the same syrup in a 1000 kg IBC with a bottom discharge valve, labelled to the mill's own specification if required.
Storage & Handling
Store indoors between 15 °C and 30 °C, upright and closed, away from dye drums and acids. Cold makes the syrup heavy to pump and can seed crystals that would score a padder roller, so warm a chilled drum to room temperature and roll it before use. Keep bungs sealed in a humid finishing room to prevent dilution, and do not store against an outside wall where condensation forms. Part-used drums should be closed and used before a new drum is opened.
Why Choose Us
Food-Grade Focus – Our sorbitol is produced to food-grade standards and meets FCC, FAO/JECFA, and EU E420 requirements, giving you confidence in product safety and regulatory compliance.
Halal & Kosher Certified – Ready for export to markets with specific certification requirements, saving you time and simplifying your import process. Sorbitol is recognized as Halal by multiple certification bodies and approved for use in Saudi Arabia, Qatar, and other Muslim-majority countries.
Consistent Quality Every Drum – Clear appearance, stable 70% concentration, and reliable performance batch after batch. Each shipment comes with a Certificate of Analysis for your records.
Flexible Wholesale Supply – From trial orders to ongoing bulk shipments, we scale to match your production needs. Whether you need one drum or a container load, we can accommodate.
Fast Delivery – We understand that timely supply matters. Our logistics are set up to get your order to you without unnecessary delays.
Responsive Support – Questions about specifications, certifications, or shipping? Our team responds quickly so you can keep your business moving.
Export Experience – We understand the documentation and compliance requirements for international food ingredient shipments and are ready to be your dependable long-term partner.